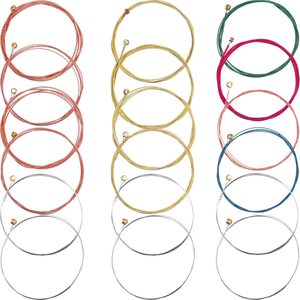
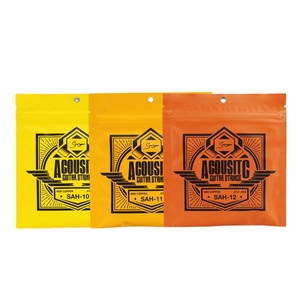
Different Style and Color Wholesale Price Acoustic Guitar Strings Sets String Guitar for Beginner
High-Tensile Hex Core | Anti-Corrosive Coating | Balanced Dynamic Tension
Explore production-ready hollow body guitars, semi-hollow conversion neck assemblies, calibrated pickup matrices, and export-grade hardware built to exacting international standards.
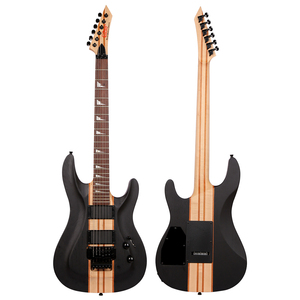
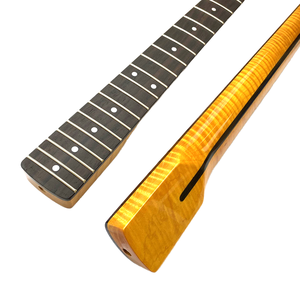
Sourcing hollow body guitars from Chinese OEM hubs demands an intricate understanding of timber hygroscopy, mechanical center-block coupling, and microphonic damping.
Full hollow archtops require specific acoustic resilience without succumbing to wolf-tones or runaway stage feedback. Our export-grade bodies utilize multi-ply maple, birch, and spruce press-molded under 40-ton pneumatic presses using high-grade urea-formaldehyde resin matrices for enduring curvature memory and harmonic snap.
For thinline and semi-hollow instruments, center-block wood choice dictates sustain characteristics. We offer precision-routed solid mahogany or weight-relieved quarter-sawn spruce core blocks. This structural spine bridges the top and back plates, dissipating microphonic air resonances while granting mounting security for stop-tailpieces and tune-o-matic bridges.
Exporting archtop guitars to regions with alternating seasonal humidity (North America, Northern Europe) requires refined edge binding and internal f-hole profiling. Every soundhole is treated with moisture-barrier sealing lacquers and internal conductive paint bays to eliminate parasitic 50/60Hz RF hum across single-coil and P-90 pickup configurations.
Evaluate body architectures, feedback mitigation thresholds, and container export parameters across standard production lines.
| Architecture Type | Acoustic Chamber Style | Primary Tonewoods | Feedback Resistance | Typical Target Market | Recommended Action |
|---|---|---|---|---|---|
| Full Hollow Jazz Archtop | Unobstructed 3.25" deep acoustic body, parallel spruce bracing | Laminated Flamed Maple Top/Back, Select Mahogany Rim | Moderate (Optimized for low-to-mid stage volume) | Boutique Jazz/Bebop, Traditional Conservatories | Get a Quote |
| Thinline Semi-Hollow | 1.75" profile with continuous solid Maple/Spruce center block | Spruce / Flame Maple Laminate, Mahogany Neck | High (Ideal for overdrive, rock, and modern indie) | Mainstream Retail Chains, Touring Rock Bands | Get a Quote |
| Chambered Hybrid Thinline | Solid mahogany back routed with acoustic pockets, solid drop-top | African Mahogany body with Carved Flamed Maple cap | Very High (Performs identically to solid-body instruments) | Session Players, Fusion Artists, Modern Studio Pros | Get a Quote |
| Nylon-String Thinline Acoustic | Slimline acoustic cavity with soundpost reinforcement | Solid Cedar or Engelmann Spruce Top, Rosewood Sides | High (Internal piezo preamp & notch filters) | Stage Performing Guitarists, Fingerstyle Virtuosos | Get a Quote |
Market shifts reshaping how international importers, distributors, and OEMs procure fretted instruments from Chinese export hubs.
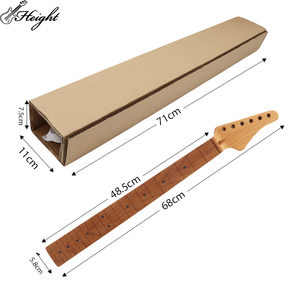
Roasted maple necks and thermo-treated spruce tops are rapidly transitioning from custom shop luxuries to core factory requirements. Thermo-curing reduces wood equilibrium moisture to near 0% before acclimating to 5%, eliminating freight warp during oceanic transit.
With stringent global customs checks on Dalbergia and endangered rosewood, Tier-1 Chinese exporters are shifting towards engineered black richlite, laurel wood, and thermally modified jatoba to guarantee clean Lacey Act and CITES documentation at port of entry.
High-speed 5-axis CNC shaping paired with computer-controlled fret leveling machines (Plek systems) has eliminated inconsistent fingerboard action across bulk runs. Buyers can now specify low-action setups directly from the factory line without secondary retail adjustments.
Environmental VOC mandates have spurred the adoption of ultra-thin, photo-initiated UV curing finishes. These coatings measure under 0.08mm in thickness, matching nitrocellulose lacquer in resonant openness while offering industrial scratch resistance and immediate container packing.
Decades of international luthiery collaboration, Japanese quality oversight standards, and robust supply alliances with world-leading component manufacturers.
Rooted in design methodologies honed since 1956 in Nagoya, our production oversight implements a strict three-tier gate inspection: raw timber equilibrium verification, post-lacquer dimensional auditing, and final luthier bench setup before palletization.
We provide end-to-end original equipment manufacturing services, from custom headstock silhouettes and bespoke pearl/abalone fretboard inlays to tailored pickup winding profiles. Our engineering team converts 2D blueprints or sample instruments into scalable CAD/CAM production lines.
As authorized global export partners and distributors for world-standard hardware leaders like GOTOH Japan machine heads and Augustine classical strings, our instruments can be factory-equipped with authentic, rider-compliant hardware without gray-market tariffs.
Essential answers for category managers, supply chain directors, and retail purchasing heads.
Standard OEM hollow body production runs typically begin at 50 to 100 units per model, allowing mixed color finishes across 2 to 3 iterations. For stock or ready-to-ship models, sample trial orders starting at single-carton quantities are available for qualified music distributors.
All export tonewoods undergo a controlled 90-day dehumidification and computerized kiln-drying cycle to achieve 8%-10% equilibrium moisture content. Finished instruments are packed in desiccant-lined, moisture-sealed polybags inside multi-wall corrugated master cartons engineered for trans-Pacific container climates.
Yes. Leveraging our official export partner status with GOTOH and close relationships with OEM pickup winders, we can equip your orders with authentic Japanese hardware, CTS potentiometers, Switchcraft jacks, or our high-grade S109 series Alnico pickups based on your cost targets.
Completely. We enforce full documentation chains for all timber origins. Finishes are heavy-metal free compliant with RoHS/REACH, and fretboards use certified Indian Rosewood or non-regulated alternative tonewoods (Roasted Maple, Technical Ebony, Laurel) with full customs clearances provided.
New private label prototypes generally require 35 to 45 days for CNC programming, mold pressing, and assembly. Following master prototype approval, mass production cycles require 60 to 75 days depending on lacquer curing styles (UV vs Polyurethane).
Every instrument undergoes a calibrated fret-rocker verification under standard string tension, checking for relief between 0.25mm and 0.40mm. Electronics are tested in an RF-attenuated listening booth to ensure zero ground loops or microphonic howl at peak volume.